Belt conveyor types and applications in manufacturing plants
A comprehensive guide
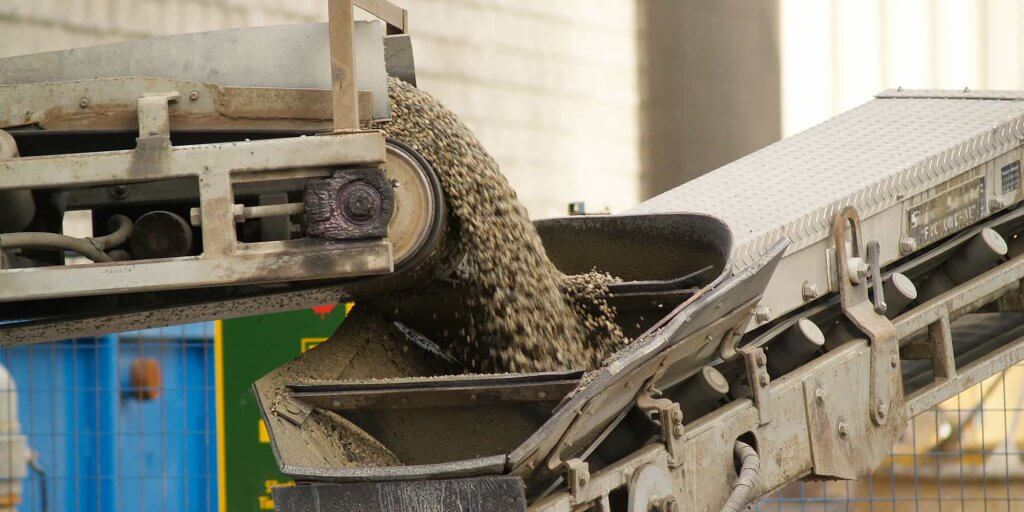
A belt conveyor moves material on a continuous loop of belting driven between pulleys. The main types of conveyor belts used in manufacturing are flat, cleated, incline/decline, curved, slider bed, roller bed, modular and sanitary washdown designs, selected by route, load and hygiene needs. Fine, dusty or high-value powders may suit an enclosed conveyor better.
The belt conveyor plays a crucial role in the industrial sector, especially in bulk material handling processes. It is a popular choice for conveying powders and granules in manufacturing plants due to its efficiency and versatility. With numerous options available in the market, it’s essential to select the right belt conveyor for your manufacturing plant.
This guide explores the different types of belt conveyors and their specific applications, providing valuable insights for senior technical plant managers.
What are the main types of belt conveyor?
Flat belt conveyor
The most common belt conveyor is the flat belt conveyor, consisting of a flat belt material stretched over several pulleys. It is used for moving materials horizontally or at a slight incline of about 15–20° (for loose bulk material) and is ideal for transporting light to medium loads.
- Application: Primarily used for horizontal or near-horizontal material transport.
- Layout suitability: Ideal for both short- and long-distance runs within a single plane. It is commonly used in assembly lines, packaging, and sorting operations where a straight path is required.
- Technical considerations: It can handle a variety of load sizes and shapes but is less effective at steep inclines due to potential slippage of materials.
Troughed belt conveyor
A troughed belt conveyor carries material on a belt that runs over angled idler rollers. The idlers bend the belt edges upward into a trough shape, which holds loose bulk material in the centre of the belt. Troughed belts are the standard design for moving high volumes of bulk material over long distances.
- Application: Troughed belt conveyors are used for high-volume bulk materials such as ores, coal, aggregates, grain, cement clinker and fertiliser, in mining, quarrying, agriculture and bulk processing plants.
- Layout suitability: They suit long, straight runs and moderate inclines, including conveying between buildings or from stockpiles to the process.
- Technical considerations: Three-roll idler sets are commonly set at troughing angles of 20°, 35° or 45°. A deeper trough carries more material and spills less, but needs a more flexible belt and a longer transition at each pulley. The top of the belt is open, so fine or dusty powders need covers or hoods to control dust.
Cleated belt conveyor
A belted conveyor has cleats or barriers on the belt surface, providing extra support for materials moving at steeper angles. This design prevents the powders or granules from sliding back.
- Application: Best suited for inclines or declines in the conveyor path.
- Layout suitability: Useful in multi-plane layouts where materials need to be transported at an angle, especially in tight spaces where a traditional incline conveyor would be too steep.
- Technical considerations: The height and spacing of cleats can be customised based on the granule size and angle of incline, ensuring minimal slippage and controlled material flow.
Incline/decline belt conveyor
Specifically designed for moving materials at an angle, this conveyor is essential in facilities where space is limited. The angle of incline is adjustable to accommodate different types of materials.
- Application: Specifically designed for vertical or steep transport of materials.
- Layout suitability: Optimal for facilities with multi-level operations where materials need to be moved between different elevations.
- Technical considerations: The steepness of the conveyor is a critical factor and is balanced with the nature of the material to prevent slide-back.
Curved belt conveyor
The curved belt conveyor is designed with a curved frame that allows the conveyor to turn corners or navigate around obstacles. It is useful in complex plant layouts where a straight conveyor would be impractical.
- Application: Utilised for changing the direction of material flow within a plant.
- Layout suitability: Effective in complex layouts where materials need to navigate around obstacles or turn corners without transferring to another conveyor.
- Technical considerations: The curvature radius needs to be large enough to prevent material spillage while maintaining belt integrity and efficiency.
Slider bed belt conveyor
In this system, the belt slides over a flat surface, reducing friction. This design is suited for longer distances and heavier loads, making it a good choice for transporting granules or powders over longer distances within a plant.
- Application: Suitable for longer, horizontal or low-incline runs.
- Layout suitability: Ideal for straight paths across long distances within a plant, such as in warehousing or distribution sections.
- Technical considerations: The friction between the bed and the belt needs to be managed, especially for heavier loads or longer distances, to ensure smooth operation and minimise wear.
Roller bed belt conveyor

A roller bed belt conveyor supports the belt on rollers rather than a slider bed. This reduces friction and allows for heavier loads and longer conveying distances. It is particularly effective for high-volume material handling.
- Application: Used for heavy loads and long-distance transport.
- Layout suitability: Appropriate for straight, long-distance routes, especially in areas like shipping and receiving or bulk material handling.
- Technical considerations: Roller support reduces belt friction and wear, allowing for heavier loads and reduced energy consumption.
Modular belt conveyor
A modular belt conveyor uses a belt made up of individual, interlocking plastic modules. It is highly durable and easy to clean, making it suitable for food or pharmaceutical manufacturing where hygiene is crucial.
- Application: Versatile, used for straight, incline, and even curved paths.
- Layout suitability: Highly adaptable to complex layouts with multiple planes and directions, including tight turns and small footprints.
- Technical considerations: Modular design allows for easy maintenance and replacement of damaged sections. The design also accommodates a wide range of product sizes and shapes.
Sanitary and washdown belt conveyor
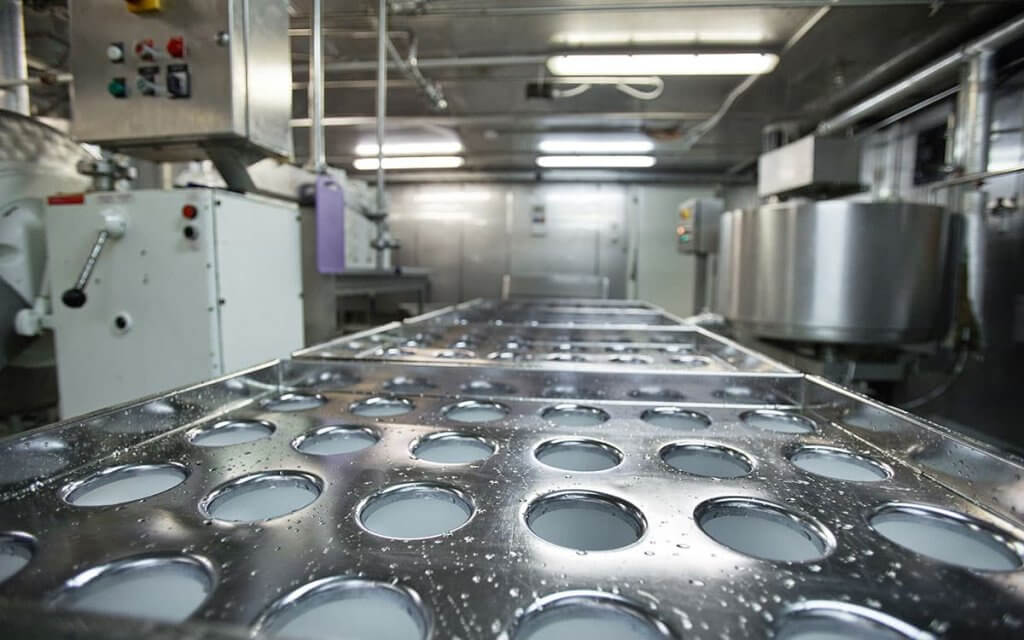
Designed for environments where cleanliness is essential, this conveyor is made with materials that can withstand rigorous cleaning protocols. It is suitable for transporting powders and granules in food, pharmaceutical, and chemical industries. While sanitary belt designs exist, open belts still expose product; fully enclosed conveying removes that exposure.
- Application: Designed for environments requiring high hygiene standards.
- Layout suitability: Commonly used in food processing, pharmaceuticals, and chemical industries where the conveyor path needs regular cleaning and sanitisation.
- Technical considerations: Made with corrosion-resistant materials and designed for easy cleaning and drainage. The layout must allow for accessibility for regular washdowns.
Each type of belt conveyor has its unique advantages and is chosen based on the specific requirements of the material being transported, the layout of the manufacturing plant, and the necessary handling capacity.
Small, mini and portable belt conveyors
Small and mini belt conveyors are scaled-down versions of standard designs, used where space is tight or volumes are low, such as small-batch packaging or pharmaceutical lines. Portable belt conveyors add mobility. Telescopic belt conveyors extend into trucks and containers for loading and unloading, and wheel- or track-mounted mobile conveyors can be moved around a site or between sites in mining, agriculture and construction. Their capacity is lower than that of fixed conveyors, so check throughput against your requirements and plan how the unit will feed into, or take from, your existing equipment.
Telescopic belt conveyors
- Application: These can be extended into trucks or other areas for loading or unloading materials, commonly used in logistics and warehousing.
- Technical considerations: The mobility and adjustability make them highly versatile for various loading and unloading tasks.
Wheel-mounted mobile conveyors
- Application: Often used in mining, agriculture, or construction where the conveyor needs to be moved over a site or between multiple sites.
- Technical considerations: These conveyors are mounted on wheels or tracks and can be easily relocated.
Key considerations
These types of conveyors are best suited for specific tasks – small and mini conveyors for light or precision tasks, and portable conveyors for temporary or dynamic operations.
Consideration also needs to be given to how these specialised conveyors will integrate with existing systems and processes. Their utility often depends on how well they complement larger systems.
What are belt conveyors made of?
Conveyor belts are built in two layers: a carcass that gives the belt its strength, and a cover that protects the carcass from the material being carried. The carcass sets how much tension the belt can take. The cover sets how well it resists wear, heat, oil and cleaning chemicals. Most conveyor belting types are a combination of the two.
Carcass materials
- Fabric-ply: Layers of woven polyester and nylon (often called EP belting) bonded with rubber. Fabric-ply is the most common construction, used for general bulk handling in quarries, grain terminals and manufacturing plants.
- Steel cord: Steel cables embedded lengthways in rubber. Steel cord belts run long, high-tension conveyors in mining and ports, where a fabric carcass would stretch too far.
- Solid woven: A single thick woven carcass impregnated with PVC or PVG.
Cover materials
- Rubber: Natural and synthetic rubber compounds handle abrasive, heavy bulk materials such as ore, aggregates and clinker, with specialist grades for heat, oil or fire resistance.
- PVC: PVC covers suit light-duty and food lines that need a smooth, low-cost surface that is easy to clean.
- Polyurethane (PU): PU covers are used in food and pharmaceutical processing, where the belt must resist oils, fats and frequent washdown.
Food-contact belts must use compliant compounds, such as those meeting FDA or EU food-contact requirements.
Surface options
- Smooth: A flat-top surface for horizontal and gently inclined runs, and the easiest to scrape clean.
- Rough-top: A textured surface that grips packaged goods on inclines, but adds little for fine powders and is harder to clean.
- Cleated or chevron: Raised profiles moulded or fixed to the belt that stop material sliding back on steeper inclines.
- Corrugated sidewall: Flexible walls along both edges, combined with cleats, that form pockets for steep or vertical lifts.
Belt conveyor types compared
| Type | Best for | Incline capability | Suitability for fine powders | Main limitation |
|---|---|---|---|---|
| Flat belt | Horizontal runs, light–medium loads | Slight incline only | Low unless enclosed - dust and carryback | Material slides back on inclines |
| Troughed belt | High-volume bulk materials over long distances | Moderate, ~15-20° depending on material | Low unless covered, open top releases dust and fines cause carryback | Belt needs a transition distance at each pulley; wide footprint |
| Cleated belt | Inclines/declines, granules | Steeper than flat | Moderate - cleats help; spillage at transfers | Cleaning between cleats |
| Incline/decline belt | Moving between levels | ~15-20° for smooth belt; ~25-30° for rough-top belt | Low–moderate | Slide-back on steep angles |
| Curved belt | Changing direction | Usually flat | Low | Spillage on tight radii |
| Slider bed | Long straight runs, lighter loads | Low incline | Low | Friction and belt wear |
| Roller bed | Heavy loads, long distances | Low incline | Low | Open design, dust |
| Modular belt | Hygiene-critical food/pharma, complex paths | Straight, incline, curved | Moderate - hinge gaps can trap fines | Fines lodging in joints |
| Sanitary/washdown | Food, pharma, chemical with washdown | Varies | Moderate | Water ingress with hygroscopic powders |
Advantages of belt conveyors
Understanding the diverse capabilities of belt conveyors is crucial in optimising bulk material handling processes.
Versatility with different materials
Belt conveyors can handle a wide range of materials, including powders, granules, and larger items. They are less likely to cause material segregation or degradation, which can be a concern with pneumatic systems.
- Gentle handling: A belt conveyor provides a smooth and consistent flow, minimising the chances of damaging fragile materials. This is a significant advantage over systems like screw conveyors, which can be more abrasive.
- Customisable for specific materials: The belt material, cleat design, and conveyor speed can be tailored to suit specific material characteristics, ensuring optimal material handling and reduced spillage.
- Reduced dust generation: Enclosed belt conveyor designs can significantly reduce dust generation, crucial for handling powders and granular materials, and for maintaining a clean plant environment.
Plant layout and route advantages
The flexibility of belt conveyors allows for innovative plant layout designs, enhancing operational efficiency.
- Flexibility in layout design: A belt conveyor can be designed to fit various plant layouts, accommodating straight, curved, inclined, or declined paths, which might be challenging for rigid systems like screw conveyors.
- Long-distance conveying capability: A belt conveyor is ideal for covering long distances within a plant, which can be less feasible or more expensive with technologies like pneumatic conveyors due to energy inefficiency over long distances.
- Space efficiency: Belt conveyors can be designed to maximise space usage, with options for overhead routing or tight turns, making them suitable for plants with limited space.
- Elevation changes: Capable of incline or decline conveying, belt conveyors can effectively move materials between different levels within a plant, which is a limitation for some conveyor types like vibrating conveyors.
- Integration and expansion flexibility: Belt conveyors can be integrated into existing production lines and can be expanded or reconfigured as plants need change. This adaptability is a significant benefit over more static systems.
Belt conveyors offer several benefits that suit many manufacturing environments.
- Cost-effectiveness: Generally, belt conveyors have lower installation and maintenance costs compared to systems like pneumatic conveyors.
- Energy efficiency: They are more energy-efficient for long-distance transport compared to pneumatic or vacuum systems.
- Ease of maintenance: Belt conveyors have simpler mechanics and easier accessibility for maintenance and repairs compared to more complex systems.
Belt conveyors and fine powders
- Dust at loading and transfer points: Fine particles become airborne wherever powder drops onto or off the belt. Skirtboards, transfer chute enclosures and dust extraction reduce the release, but they add cost and maintenance, and dust still escapes along an open carrying run.
- Carryback: Fine and slightly damp powders cling to the belt surface and are carried past the discharge point. The residue falls off along the return run, building up under the conveyor and around the idlers. Belt scrapers help, but they need regular adjustment and replacement.
- Moisture pickup: Hygroscopic powders such as sugar, salt and some chemicals absorb moisture from the air on an open belt. The result is caking, build-up on the belt and inconsistent flow downstream.
- Segregation of blends: Blended powders can separate by particle size and density as they settle on the belt, and again as they leave the head pulley. A mix that left the blender uniform may not arrive that way.
- Combustible dust: Many organic and metallic powders are combustible. Dust clouds at transfer points, combined with static or hot bearings, create an ignition risk. That risk has to be assessed under the relevant hazardous area requirements, such as ATEX or IECEx.
Covers and hoods on a belt conveyor solve some of these problems. Where they can’t, a fully enclosed conveyor is usually the more practical option. Aero-mechanical conveyors and tubular drag conveyors move powder inside a sealed tube, so dust stays contained, moisture stays out and blends arrive intact, at any angle including vertical.
When is a belt conveyor the wrong choice?
While belt conveyors are versatile and widely used in bulk material handling, there are specific scenarios where they may not be the best choice.
- Excessive load weight: Belt conveyors have a maximum load capacity. Extremely heavy loads can strain the conveyor belt, leading to increased wear, potential breakdowns, or the need for more robust and costly conveyor systems.
- Highly abrasive materials: If the materials being transported are highly abrasive, they can wear down the conveyor belt quickly, necessitating frequent replacements and increasing maintenance costs.
- Very high temperatures: Standard conveyor belts are typically rated to about 60-80°C; heat-resistant grades extend this to about 120-150°C.
- Wet or sticky materials: Materials that are wet, sticky, or have a tendency to clump can adhere to the belt surface, causing cleaning and maintenance challenges. This can disrupt the conveyor’s efficiency and lead to more frequent stoppages for cleaning.
- Chemically reactive materials: Certain chemicals or materials might react with the material of the conveyor belt, leading to degradation or damage. In such cases, specialised materials are required, which might be more expensive or difficult to source.
- Sharp or jagged materials: Sharp or jagged objects can cut or tear the conveyor belt, especially if the belt is not designed for such materials. This can lead to frequent belt replacements and increased downtime.
- Complex bulk material handling requirements: While belt conveyors are adaptable, they might not be the best choice for extremely complex routing requirements, like those requiring frequent changes in direction or elevation within a very confined space.
- Explosive or flammable materials: The motion of the conveyor belt can generate static electricity, which could be a hazard when transporting flammable or explosive materials unless specific safety measures are in place.
- Sanitary and cleanroom environments: In environments where absolute cleanliness is necessary, such as in certain pharmaceutical or food processing applications, the nooks and crannies in conveyor belts and frames can harbour bacteria or contaminants.
- Outdoor or uncontrolled environments: Belt conveyors are less suited for outdoor use where they can be exposed to weather elements like rain, snow, or extreme temperatures, unless they are specifically designed for such conditions.
In each of these cases, alternative bulk material handling systems might be more appropriate, such as pneumatic systems for complex routes or high-temperature materials, bucket elevators for vertical transport of larger granules and lumps, or screw conveyors for wet, sticky, or chemically reactive materials, or aero-mechanical conveyors for sealed conveying and the preservation of valuable materials. The suitability of a belt conveyor system largely depends on the specific material characteristics, environmental conditions, and the operational requirements of the plant.
How to choose the right belt conveyor for your plant
Implementing a belt conveyor system requires a strategic approach, considering various factors for optimal performance.
Assess material characteristics
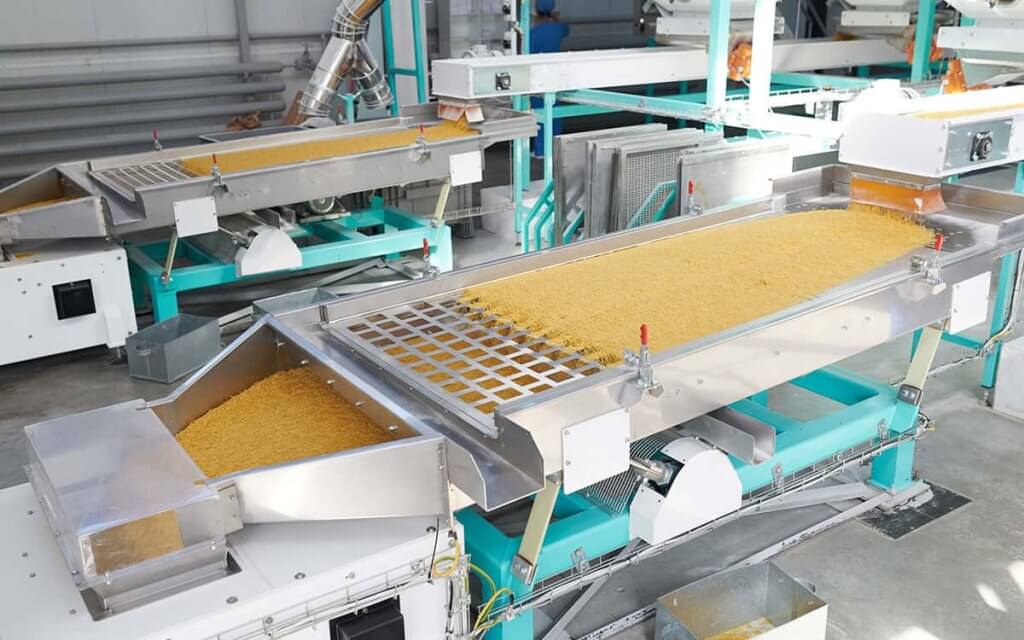
- Understand the properties: Evaluate the physical properties of the materials being handled (e.g., size, abrasiveness, stickiness, temperature sensitivity) to select the appropriate belt material and design.
Consider material impact: Factor in how the conveyor will affect the material, especially if it’s fragile, prone to degradation, or reactive.
Analyse plant and layout space constraints
- Map the route: Plan the conveyor path, considering existing structures and machinery. Belt conveyors offer flexibility, but it’s crucial to design an efficient route.
- Space utilisation: Optimise space, especially in confined areas. Vertical or inclined conveyors can save floor space.
Evaluate long-term operational costs
- Energy consumption: Consider the energy efficiency of the conveyor system, especially for long runs, as this impacts ongoing operational costs.
- Maintenance requirements: Regular maintenance is key for longevity. Choose a design that simplifies maintenance tasks and minimises downtime.
Prioritise safety and compliance
- Safety features: Incorporate safety guards, emergency stops, and other features to protect workers.
- Regulatory compliance: Ensure the conveyor system complies with industry-specific regulations, particularly in food, pharmaceutical, or chemical industries.
Customise for specific needs
- Modular design: Opt for a modular conveyor design that allows for easy expansion or reconfiguration
- Tailor for bulk material handling: Customise the conveyor (e.g., belt type, cleat design) based on the specific materials to be handled.
Consider integration with existing systems
- Seamless integration: Ensure the conveyor can be integrated smoothly with existing production lines or material handling systems.
- Automation compatibility: Check if the conveyor can be linked with automation systems for streamlined operations.
Plan for future scalability
- Adaptability: Choose a system that can grow or change with your plant’s future needs. This could involve extending the conveyor length, increasing capacity, or altering the route.
Assess environmental impact
- Dust and contamination control: If handling powders or granules, consider enclosed conveyors to minimize dust and contamination.
- Noise levels: Evaluate the noise generated by the conveyor and its impact on the work environment.
Consult with conveyor specialists
Engage with conveyor experts or manufacturers early in the planning phase to leverage their expertise in bulk material handling conveyor designs and material handling.
Cost-benefit analysis
Perform a detailed cost-benefit analysis, considering not only the initial investment but also long-term operational and maintenance costs.
Quality and durability of components
Invest in high-quality components to reduce long-term costs associated with repairs and replacements.
Belt conveyor FAQs
The flat belt conveyor is the most common conveyor system in manufacturing. A continuous belt runs over a slider bed or rollers between two pulleys, moving material horizontally or up a gentle incline. For loose bulk materials such as grain or sand, the troughed belt conveyor is standard, because its curved profile carries more with less spillage.
Read more: Comparing conveyor types
A conveyor belt is the belting itself: the continuous loop of rubber, PVC, fabric or steel-reinforced material that carries the load. A belt conveyor is the whole machine, including the belt, frame, pulleys, idlers or slider bed, drive and take-up. People often use the terms interchangeably, but specifications and suppliers treat them separately.
The maximum incline depends on the belt surface and the material. As a guide, smooth belts manage about 15–20° with bulk materials, chevron belts about 30–35°, cleated belts about 45–60°, and corrugated sidewall belts up to vertical. Fine, free-flowing powders sit at the low end of these ranges because they slide back more easily.
Read more: Vertical conveyor for flour production
Belt conveyors can move powders, but open belts are often a poor fit for fine or dusty products. Dust escapes at loading and transfer points, fines cling to the belt as carryback, and blends can separate at discharge. Enclosures and belt scrapers reduce these problems. Where they don’t, a fully enclosed conveyor is often the better option.
Read more: Dust-free powder transfer for a plasterboard line
Most conveyor belts have two parts: a carcass that gives the belt its strength, and a cover that protects it. The carcass is usually polyester or nylon fabric, or steel cord for heavy-duty runs. Covers are rubber for abrasive bulk materials, PVC or polyurethane for food and light-duty lines, and specialist grades for heat, oil or fire resistance.
Read more: ISO 14890:2026
Choosing between a belt conveyor and an enclosed conveyor
Selecting and designing a belt conveyor system requires a holistic approach, considering material properties, plant layout, operational efficiency, safety, and regulatory compliance. Customisation and flexibility are key to ensuring that the conveyor system not only meets the current needs but can also adapt to future changes and expansions. Consultation with specialists and thorough planning are essential for implementing the right bulk materials handling conveyor system for your plant.
If you’re considering a conveyor system for your next bulk powder or granule handling project, get in touch with Floveyor. As powder handling specialists with a long history, we can help you determine the best conveyor for your manufacturing plant.
 English
 Chinese
 Dutch
 Finnish
 French
 German
 Hindi
 Japanese
 Korean
 Malay
 Polish
 Spanish
 Thai
 Vietnamese